Aerospace · Drawing-based custom machining
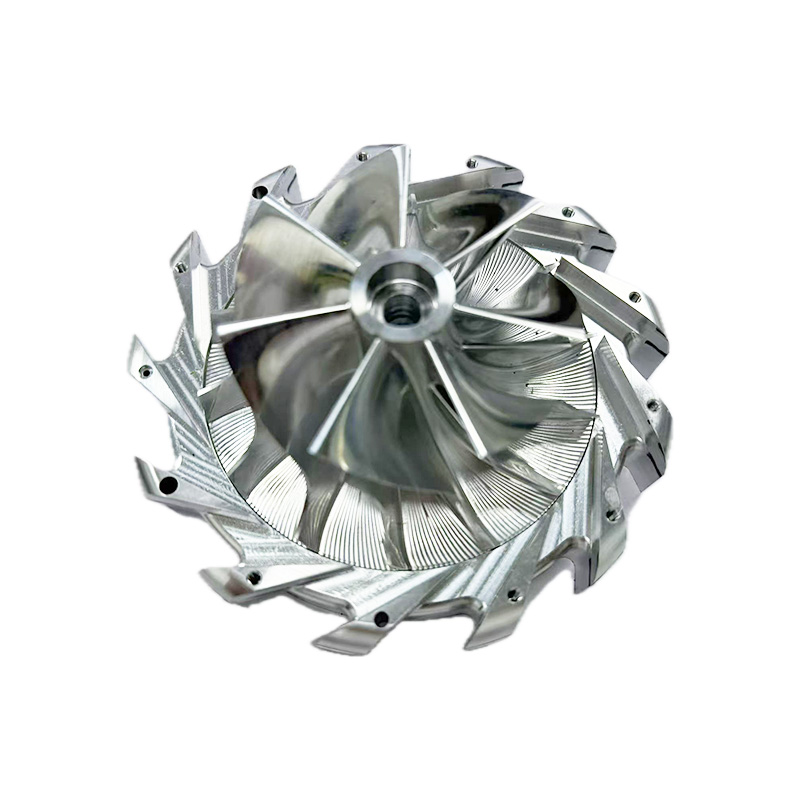
CNC Machined Impeller: Application & Engineering Review
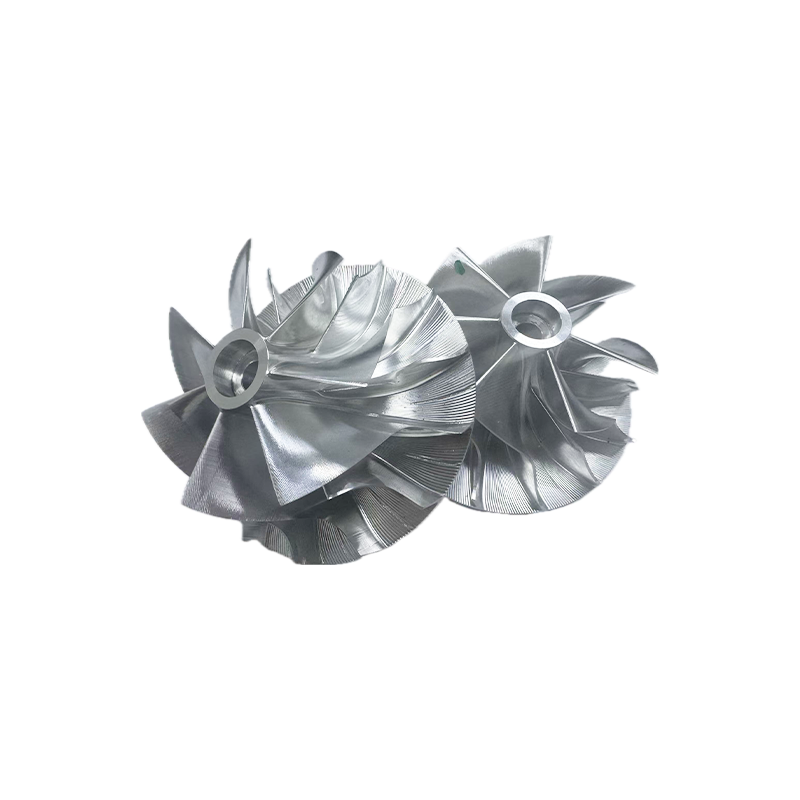
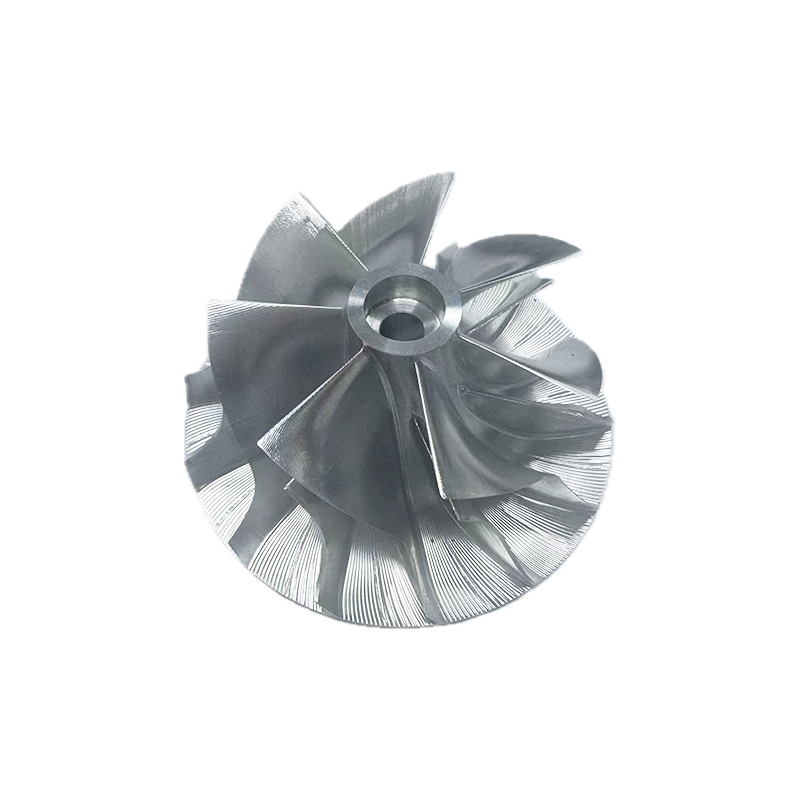
Complex bladed geometry for a reviewed airflow or rotating assembly project. This component geometry is presented to help engineering and purchasing teams specify a custom part. Final material, dimensions and suitability are defined by your approved design.
What problem should this part solve?
Thin blades, deep channels and hub interfaces require tool access, stable workholding and an agreed profile check. Start with the functional interfaces so that manufacturing and inspection work from the same acceptance criteria.
Material, process and inspection plan
| Application | Complex bladed geometry for a reviewed airflow or rotating assembly project. |
|---|---|
| Manufacturing route | Five-axis CNC roughing and finishing followed by controlled deburring of blade edges. |
| Material options to review | Specify aluminum alloy or another approved grade against speed, temperature and design qualification. |
| Surface finish to specify | Approved as-machined finish or compatible protection; define hub and blade-edge requirements separately. |
| Critical inspection features | Hub bore, blade profile and critical thickness. Balance requirements and acceptance method must be agreed separately. |
| Dimensions & tolerance | Made to the approved customer drawing. Supply overall dimensions in mm, datums, fits and feature-specific tolerances; final capability is confirmed after engineering review. |
| Prototype & production | Quote sample and repeat-order quantities separately. Lead time, inspection documents and delivery scope are confirmed in the quotation. |
Machining difficulty and practical solution
Five-axis CNC roughing and finishing followed by controlled deburring of blade edges. Hub bore, blade profile and critical thickness. Balance requirements and acceptance method must be agreed separately are the features to prioritize in the setup and inspection plan. Review tool access and workholding before freezing the drawing; agree any secondary operation rather than assuming it is included.
RFQ and sample approval checklist
Provide the CAD model and revision-controlled drawing, exact material grade, hub bore, blade profile and critical thickness. Balance requirements and acceptance method must be agreed separately, required finish and prototype/production quantities. Identify the features that control assembly and state the reports needed for release.
- Approve the first-piece measurement scope and the applicable drawing revision.
- Confirm material documents, final finish and packaging needed for your assembly.
- Review the sample against mating parts before approving repeat production.
Can LXCET review a custom version?
Send your drawing for a feasibility review of five axis CNC impeller machining. The equipment and process guide explains listed machine ranges; the quality and inspection page explains how to define acceptance evidence. A machine’s travel or listed precision value is not a universal finished-part tolerance.
Request a Drawing Review → tonyzhou@lxcet.com
Related Aerospace components
Technical reference and image scope
Aerospace programs require their own material, inspection and qualification requirements; industry association does not establish approval. Protolabs aerospace machining overview.
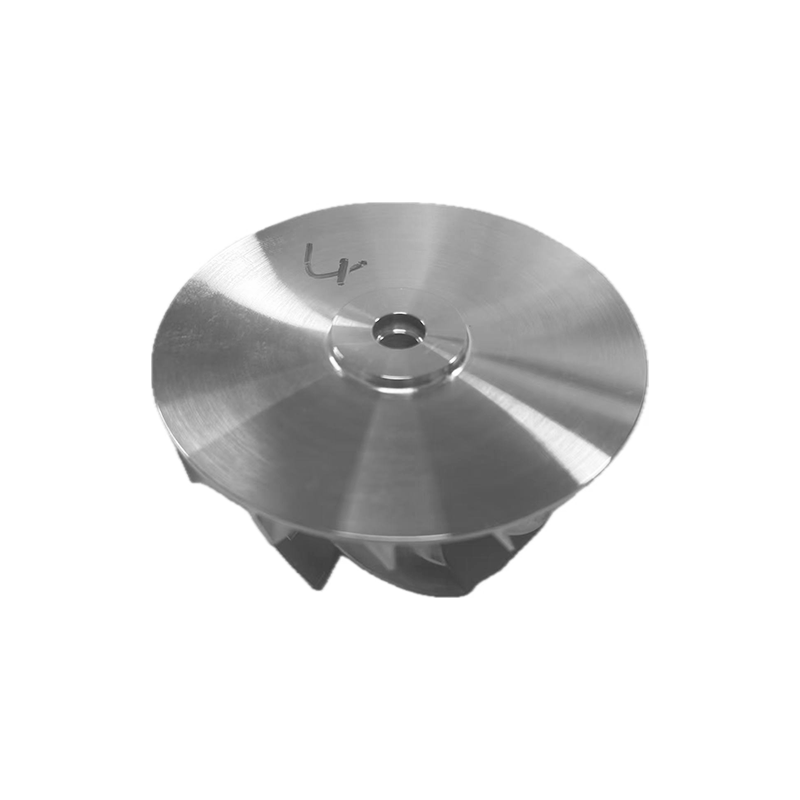
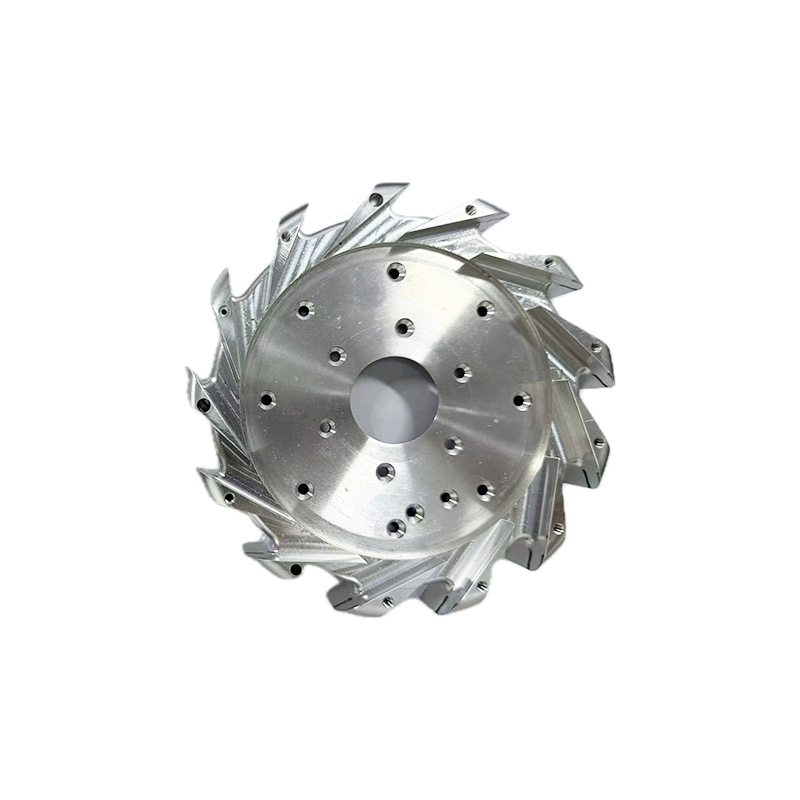
Product photograph from the existing LXCET media library. Application descriptions are engineering review examples, not claims of a delivered customer program, certification or tested service rating. Material cannot be verified from appearance alone.