Blog

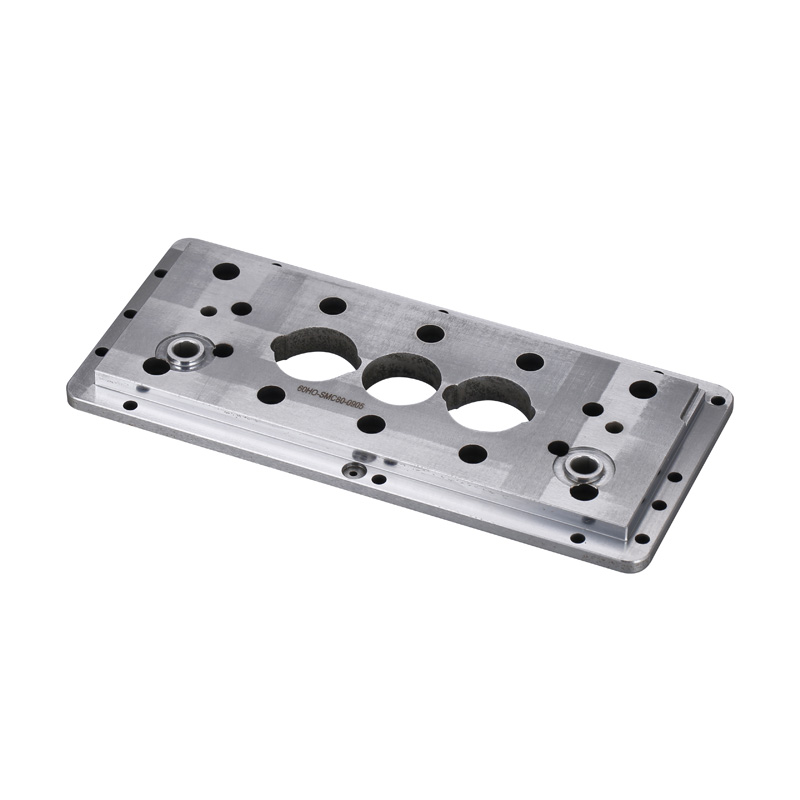
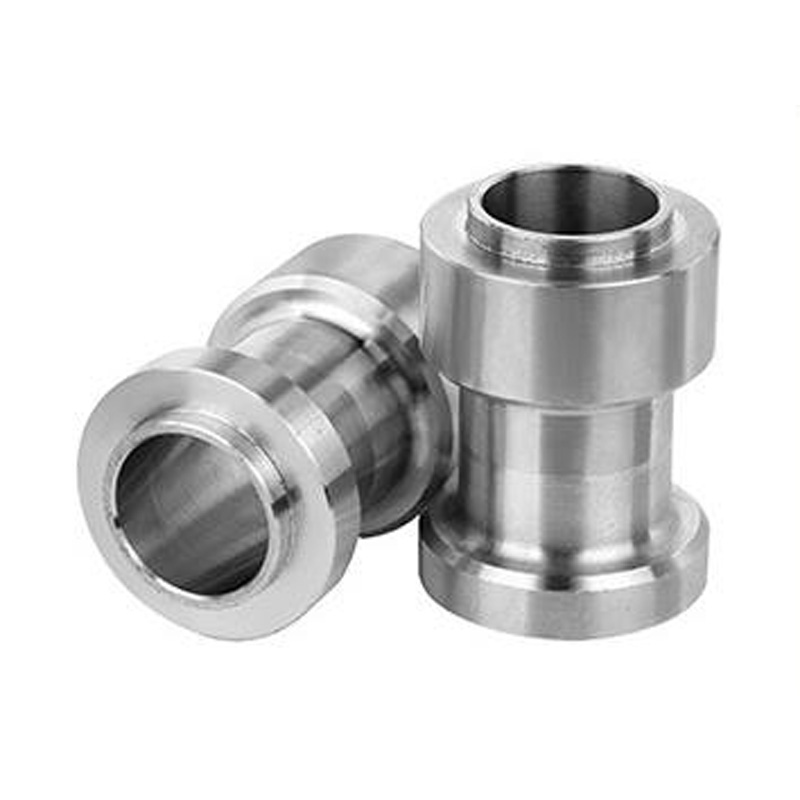
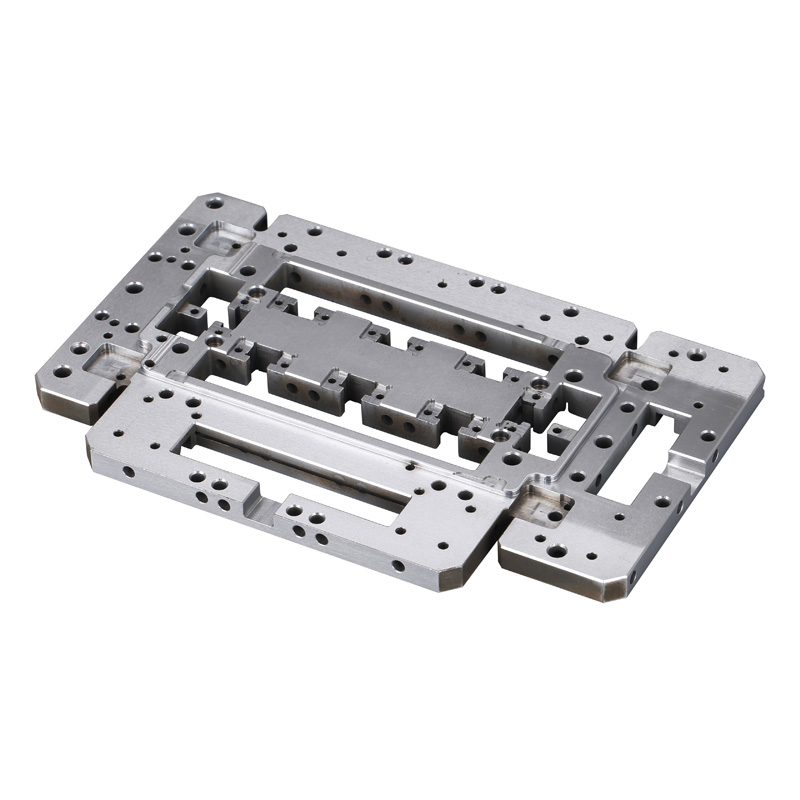
CNC machining materials include aluminum, steel, stainless steel, copper alloys, titanium, cast iron and engineering plastics. The useful question is not simply which materials can be cut. It is which grade and condition will meet your part’s operating requirements without creating unnecessary machining, finishing or inspection cost.
This guide helps engineers and buyers build a practical material shortlist. Material families are discussed for general engineering reference; availability and suitability for an LXCET project must be confirmed against the drawing.
Start with the part’s working conditions
Record load, stiffness, weight, temperature, corrosion exposure, electrical requirements and service life before comparing prices. Then identify the interfaces that actually control function: a bearing seat, a threaded connection, a sealing face or a locating datum. Separate those requirements from cosmetic surfaces.
Specify an exact grade, material standard and temper or hardness condition. “Aluminum,” “stainless” and “plastic” are incomplete purchasing descriptions. If an alternative grade is acceptable, require written engineering approval before substitution.
CNC machining materials: a practical comparison
| Material family | Typical design reason | Issue to resolve before ordering |
|---|---|---|
| Aluminum, including 6061 and 7075 | Low mass; housings, brackets and structural components | Exact temper, load requirements, corrosion exposure and finishing |
| Carbon and alloy steel | Shafts, mechanical supports and load-bearing parts | Hardness, heat treatment sequence and rust protection |
| Stainless steel, including 304 and 316L | Corrosion-conscious designs and durable fixtures | Actual environment, grade and required surface condition |
| Brass, bronze and copper | Threaded fittings, sliding components or electrical and thermal functions | Alloy-specific conductivity, machinability and composition restrictions |
| Titanium and nickel alloys | Demanding strength, corrosion or temperature requirements | Justification for the grade, machining route and qualification requirements |
| Cast iron | Rigid machine components made from cast blanks | Casting quality, machining allowance and grade-specific tool wear |
| POM, PA, PEEK and PTFE | Low mass, insulation, sliding behavior or chemical compatibility | Moisture, temperature, creep and dimensional stability |
6061 vs 7075 aluminum: choose by function
Hydro describes 6061 as a heat-treatable magnesium-silicon alloy with good corrosion resistance and useful machining characteristics. It is a sensible candidate to evaluate for general-purpose housings and brackets. Higher-strength 7075 may suit a load-driven design, but the exact temper, corrosion behavior and joining requirements still need review. A stronger alloy does not automatically make a thin wall sufficiently stiff. Compare the actual datasheets and calculate the loads rather than selecting by reputation. See Hydro’s 6061 alloy guidance and 7075 overview.
Steel, stainless steel and difficult-to-cut alloys
Steel hardness and heat treatment affect the machining route. Austenitic stainless steel can generate heat and work hardening; titanium and heat-resistant alloys place additional demands on tooling. Cast iron behavior also varies by grade. These differences help explain why two parts with identical geometry can have different production costs. Sandvik Coromant’s workpiece material guide explains these machining groups.
For a hardened shaft, define the final hardness and which dimensions must be inspected after treatment. For a stainless fixture, identify the cleaning chemicals and corrosion environment before approving a grade. Do not assume that the word “stainless” guarantees compatibility with every environment or qualifies a finished component for regulated use.
Brass and copper: conductivity and cutting behavior differ
Free-cutting brass can machine very differently from high-conductivity copper. The Copper Development Association notes that copper alloy machinability ratings are comparisons and actual operations can produce different results. Select the alloy for its functional properties first, then review chip control and finishing. For a conductive contact, define the conductivity requirement and contact surface treatment. For a threaded fitting, define thread geometry and the applicable material-composition requirements. Refer to the CDA copper rod alloy guide.
Engineering plastics: plan for dimensional movement
POM is commonly evaluated for accurately machined plastic components. PEEK offers a stiff option for demanding designs, while PTFE’s softness makes machining more difficult. Nylon’s moisture response and internal stress in plastic stock can affect the finished dimensions. Ensinger discusses these issues in its machinable plastics guide and dimensional stability guidance.
Define the operating environment and measurement conditions for a precision plastic part. A room-temperature inspection does not demonstrate that a bore will hold the same fit after moisture uptake or sustained loading. Ask whether material conditioning, stress relief or an application test is needed.
Solutions to common material selection problems
- A thin housing distorts: review stock condition, wall thickness, workholding and the roughing-to-finishing sequence before tightening every tolerance.
- A coated bore no longer fits: state whether dimensions apply before or after coating, and identify surfaces that require masking.
- A plastic part passes inspection but changes in service: compare temperature and humidity during inspection with real operating conditions; validate the fit in that environment.
- The quotation is unexpectedly expensive: separate essential material requirements from preferences, consider approved standard stock sizes and request clearly identified alternatives.
Material information to include in a CNC machining RFQ
- CAD model, controlled drawing revision, units and quantity.
- Exact grade, standard, temper or hardness and permitted substitutions.
- Critical dimensions, datums, fits and surface roughness.
- Heat treatment, coating, masking and final inspection condition.
- Required material certificates, traceability and inspection records.
- Service environment and delivery target.
Compare material choices with sourcing decisions in our guide to CNC machining in China. You can also review our 316L fixture part example.
Discuss your drawing with LXCET: send the material specification and the features that control fit and function through our CNC machining quote form. Material availability, processing route, inspection scope and delivery timing should be confirmed for the specific project.