Stainless Steel Passivation for Machined Parts: Specify and Verify

0
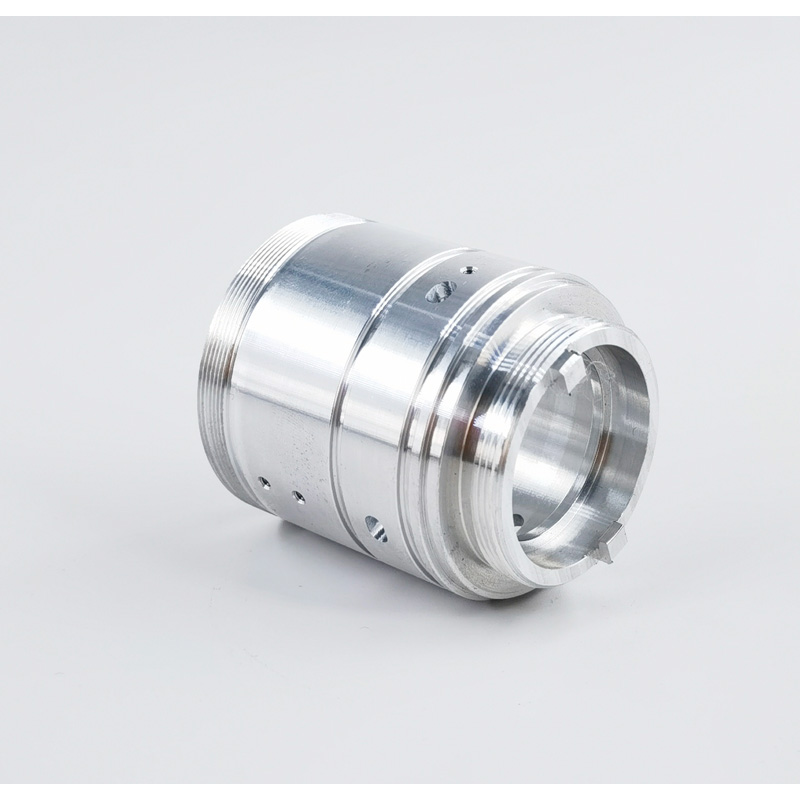
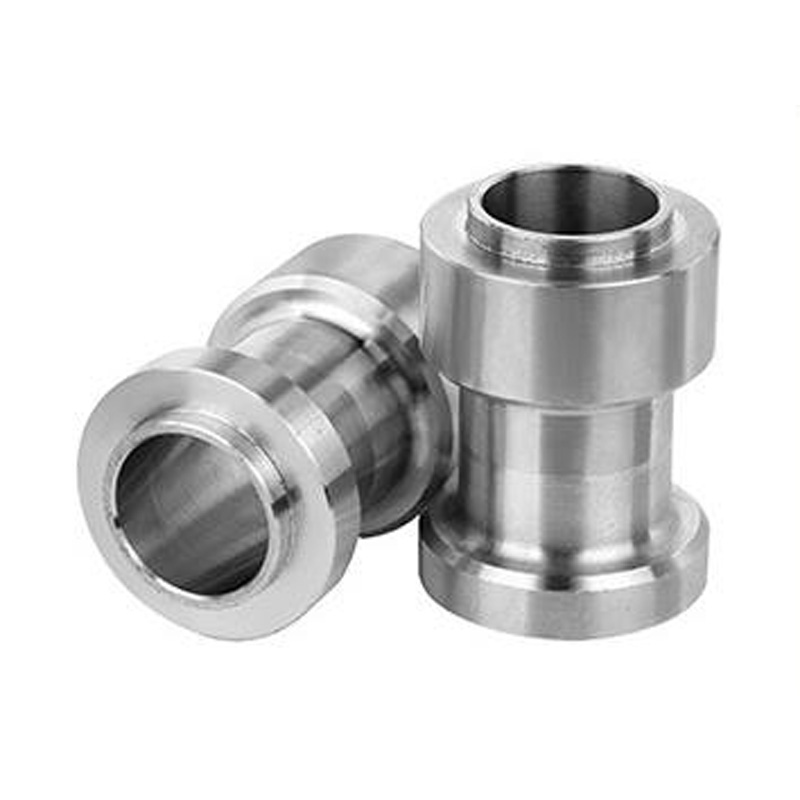
Stainless steel turned sleeves with stepped diameters and machined bores

A machined stainless steel sleeve looks clean at inspection, yet develops rust-colored spots during storage. The buyer asks for passivation, but the drawing says only “stainless steel.” Stainless steel passivation for machined parts starts with a defined alloy, surface condition and acceptance method. A shiny surface alone cannot establish corrosion performance.

Practical answer: specify the material grade and required finishing sequence, identify the applicable passivation specification and agree verification appropriate to that grade. Keep cleaning, scale removal and passivation as separate review items. Passivation does not compensate for an unsuitable alloy or establish that a component will survive every service environment.

What the surface appearance cannot tell you

Carpenter Technology explains that machining and shop handling can introduce free iron onto a stainless surface. Such contamination may rust even when the component initially appears bright. Its guide to passivating stainless parts also emphasizes cleaning before treatment and matching the verification method to the alloy.

This is a reason to investigate, not a diagnosis from a photograph. Record where the marks occur, whether they appeared before packing, the material certificate, handling history and the exposure involved. A localized stain near an embedded particle and attack associated with the operating environment may need different corrective actions. Preserve affected samples for the responsible technical team.

Specify stainless steel passivation for machined parts as a controlled operation

The current ASTM A967/A967M-25 public scope covers several chemical passivation treatments and alternative effectiveness tests. It identifies nitric, citric and electrochemical treatment routes. The full applicable specification, purchase requirements and the processor’s approved procedure determine which route and checks apply; the public abstract is not a complete process instruction.

Give the finishing supplier the actual alloy designation and condition, rather than “stainless” or a guessed family. Ask the supplier to confirm suitability of the proposed process for the part and requirements. Avoid copying a chemical recipe from an unrelated alloy into an RFQ. Detailed bath parameters belong in the controlled processing procedure.

Keep the finishing stages in the right order

Review whether the surface has oil, coolant, abrasive residue, scale or heat tint before agreeing the route. Cleaning removes unwanted material; other surface preparation may be needed before passivation is effective. Ask the processor to distinguish the work included in its quotation instead of treating one word on the drawing as a complete finishing plan.

If another machining operation is planned after treatment, identify which surfaces it will disturb and whether treatment or verification must be repeated. For an assembly, establish whether components are processed separately or together, and check access, trapped liquid and rinsing concerns with the processor. Do not assume a process qualified for an open sleeve transfers unchanged to a closed assembly.

Finding or requirementQuestion to resolveEvidence to request
Rust-colored marks after storageIs contamination, handling, packing or service exposure involved?Material identity, surface history and assessment of retained samples
Drawing calls for passivationWhich specification, edition and approved route control?Process identification and documented completion
Oil, scale or heat tint remainsWhat cleaning or preparation is needed first?Agreed initial condition and preparation scope
A free-machining grade is specifiedAre treatment and verification appropriate to that alloy?Processor review and applicable test selection
The part must be clean for final assemblyWhat residues, handling and packaging are acceptable?Separate cleanliness and packaging acceptance requirements

Agree verification before the parts reach inspection

ASTM A967/A967M describes alternative effectiveness tests. Do not order every named test by default or assume a result from one test predicts service life. State the selected method, applicable acceptance criteria and sampling or lot requirements under the controlling specification. Have the responsible technical team resolve any uncertainty about material suitability.

The report should identify the part number and revision, alloy, processed lot, specification and treatment designation, processing date and required verification results. Check that the reported lot is connected to the delivered quantity. A generic certificate without that connection leaves the buyer unable to establish which parts were processed.

Keep dimensional and cosmetic acceptance explicit as well. If a sealing surface, precision bore or appearance class matters, define its final requirements and inspection stage. A passivation statement should not replace the part’s dimensional report or the agreed surface-finish checks.

RFQ checklist for stainless components

  • Material grade, condition, traceability and controlled drawing revision.
  • Surfaces requiring treatment and any prohibited operations or masking requirements.
  • Required cleaning or preparation before passivation.
  • Applicable specification and edition, with unresolved treatment choices highlighted.
  • Verification method, acceptance criteria, lot definition and report requirements.
  • Final dimensional, finish and cleanliness requirements.
  • Handling, protective packaging and storage conditions after treatment.

Review the finished condition with the drawing

Use the inspection planning page and material certificate checklist to assemble the evidence you need. Send the grade, drawing, quantity and treatment requirement to tonyzhou@lxcet.com or the drawing enquiry form. The available finishing route and acceptance scope require project-specific confirmation.

Leave a Reply

Your email address will not be published. Required fields are marked *