Blog


Related posts
3-Axis vs 4-Axis vs 5-Axis CNC Machining: Choosing the Right Route for Your Part

Axis count is not a quality score. Here is how to match the machine route to your part geometry, and where a higher axis count actually costs you money.
CNC Machining vs Die Casting for Aluminum Parts: Cost, Tolerance and Volume Trade-offs
Aluminum parts can be machined from billet or cast to near-net shape. The right answer depends on volume, wall thickness and how tight your critical features are.
Machined Parts Packaging Requirements: Prevent Transit Damage
Define machined parts packaging requirements for surface protection, corrosion prevention, pack quantities, traceability and receiving checks.
Stainless Steel Passivation for Machined Parts: Specify and Verify
Specify stainless steel passivation for machined parts with clear alloy, preparation, verification, traceability and final-condition requirements.
Machined Part Revision Control: Prevent Wrong-Revision Orders
Prevent wrong-revision machined parts. Align CAD, drawings, purchase orders, work-in-progress decisions and inspection evidence before releasing a change.
Welding Distortion Control: Keep Mounting Faces Aligned
Control welding distortion with a practical review of weld sequence, restraint, mounting datums and acceptance checks after cooling and fixture release.
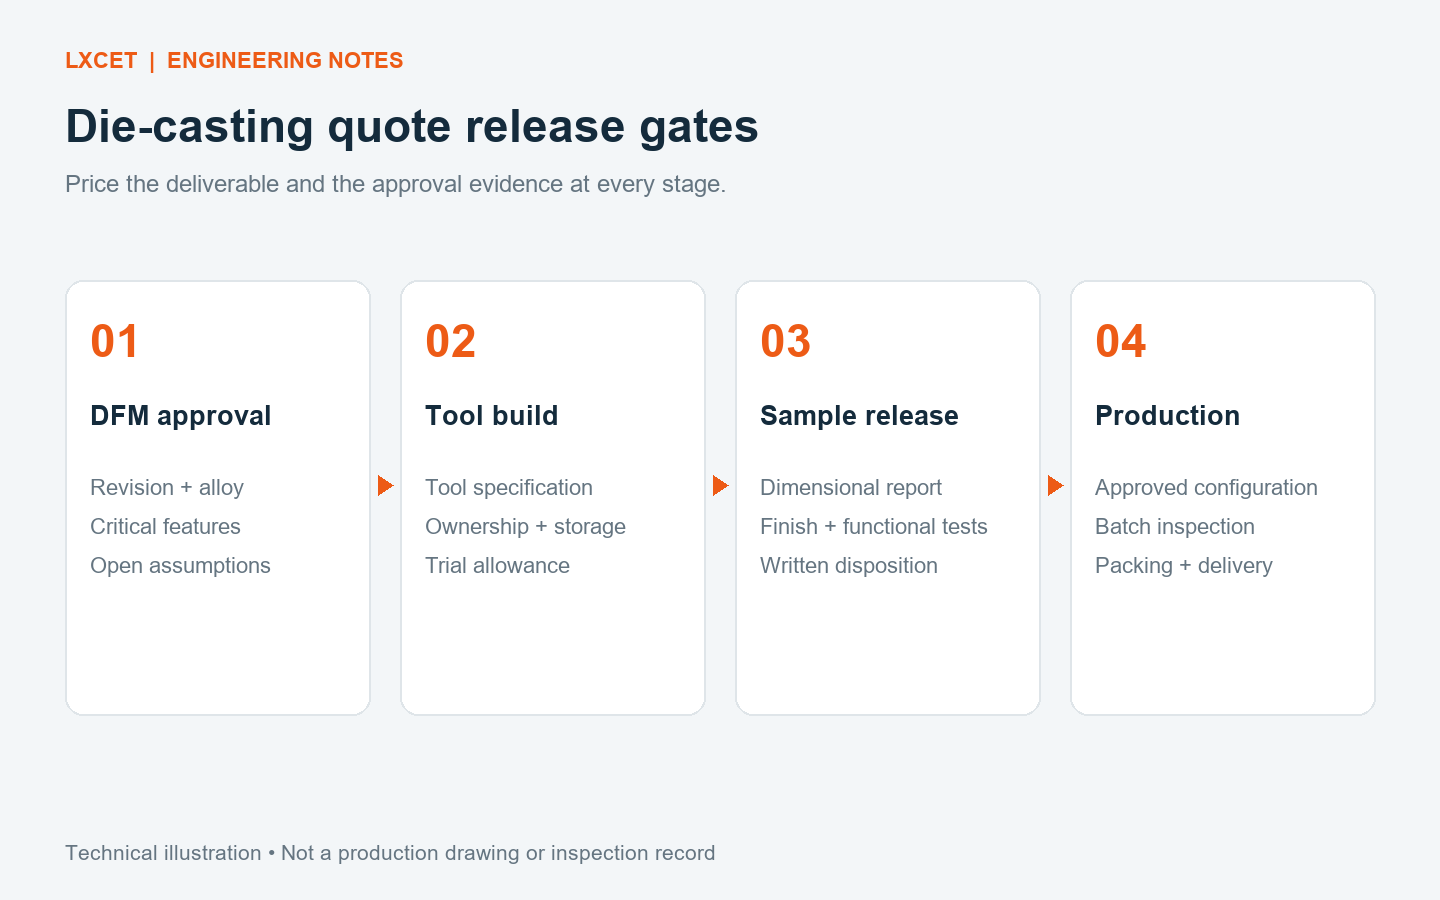
Die Casting Tooling Quote Checklist: Compare the Full Project Scope
Use this die casting tooling quote checklist to compare mold scope, trials, ownership, secondary machining, sample approval and delivery milestones.
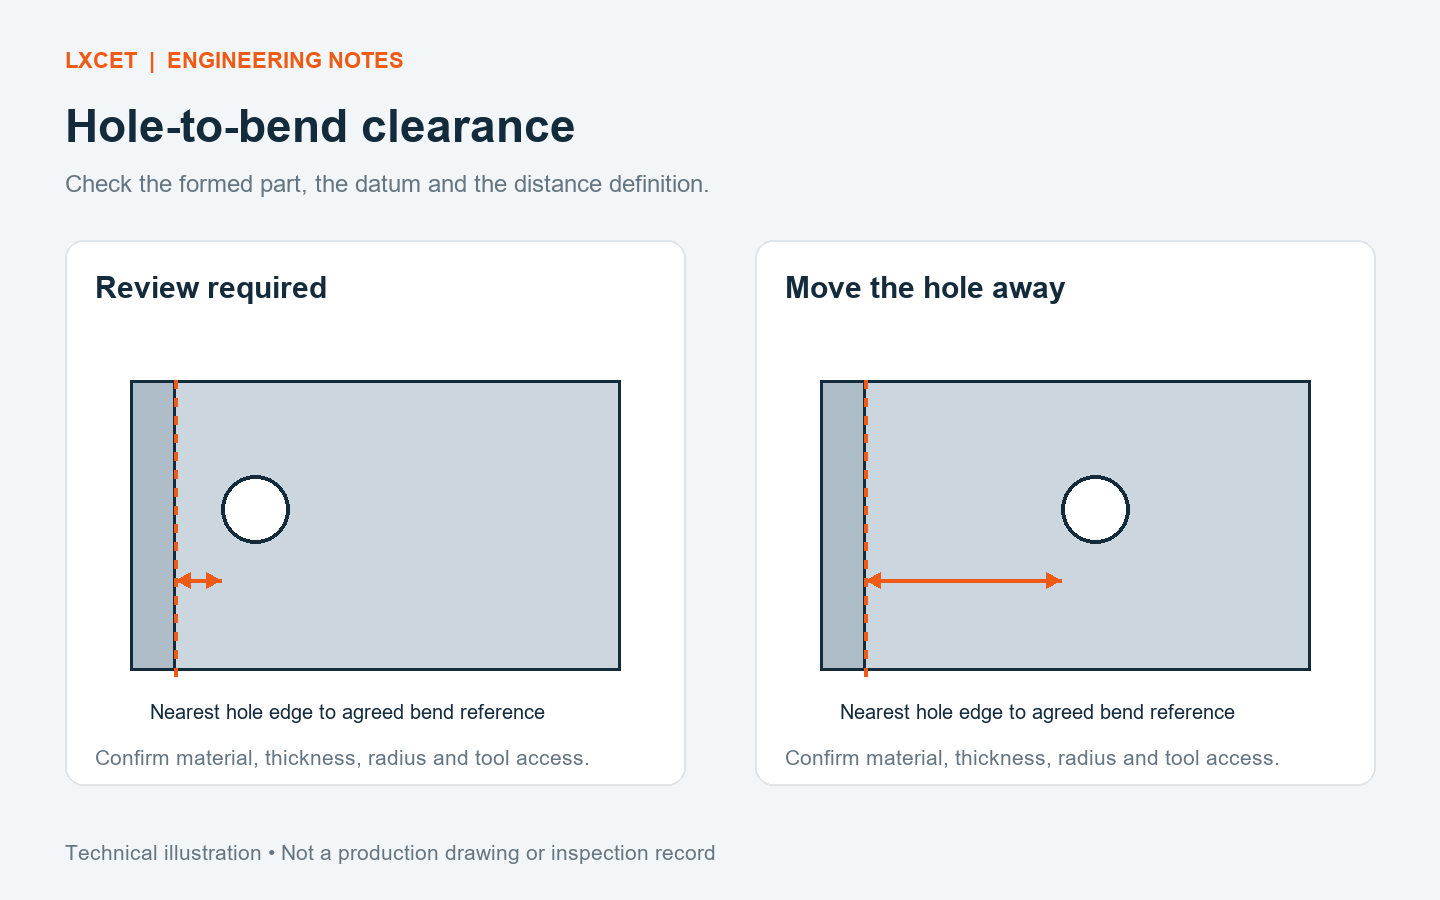
Sheet Metal Hole-to-Bend Distance: Prevent Distorted Mounting Holes
Review sheet metal hole-to-bend distance, choose a practical fix for distorted holes, and define formed-part inspection before releasing a bracket for production.
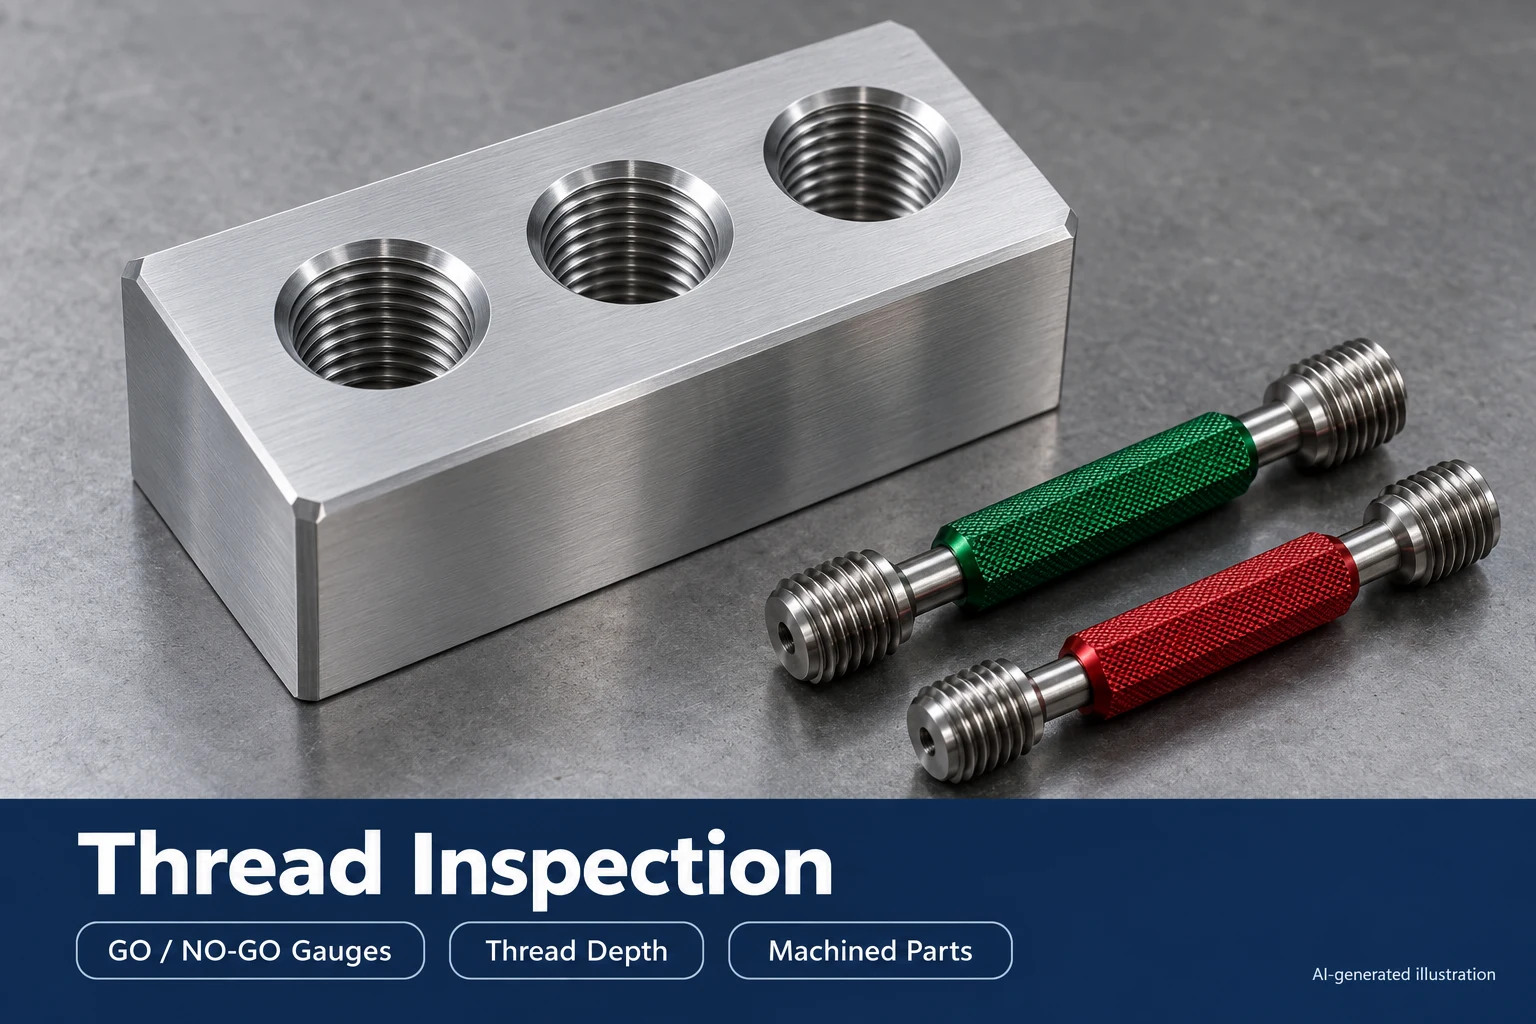
Thread Inspection for Machined Parts: A Buyer’s Acceptance Guide
Define thread class, usable depth, final finish and GO/NO-GO inspection before ordering machined parts. Includes an RFQ table and acceptance checklist.
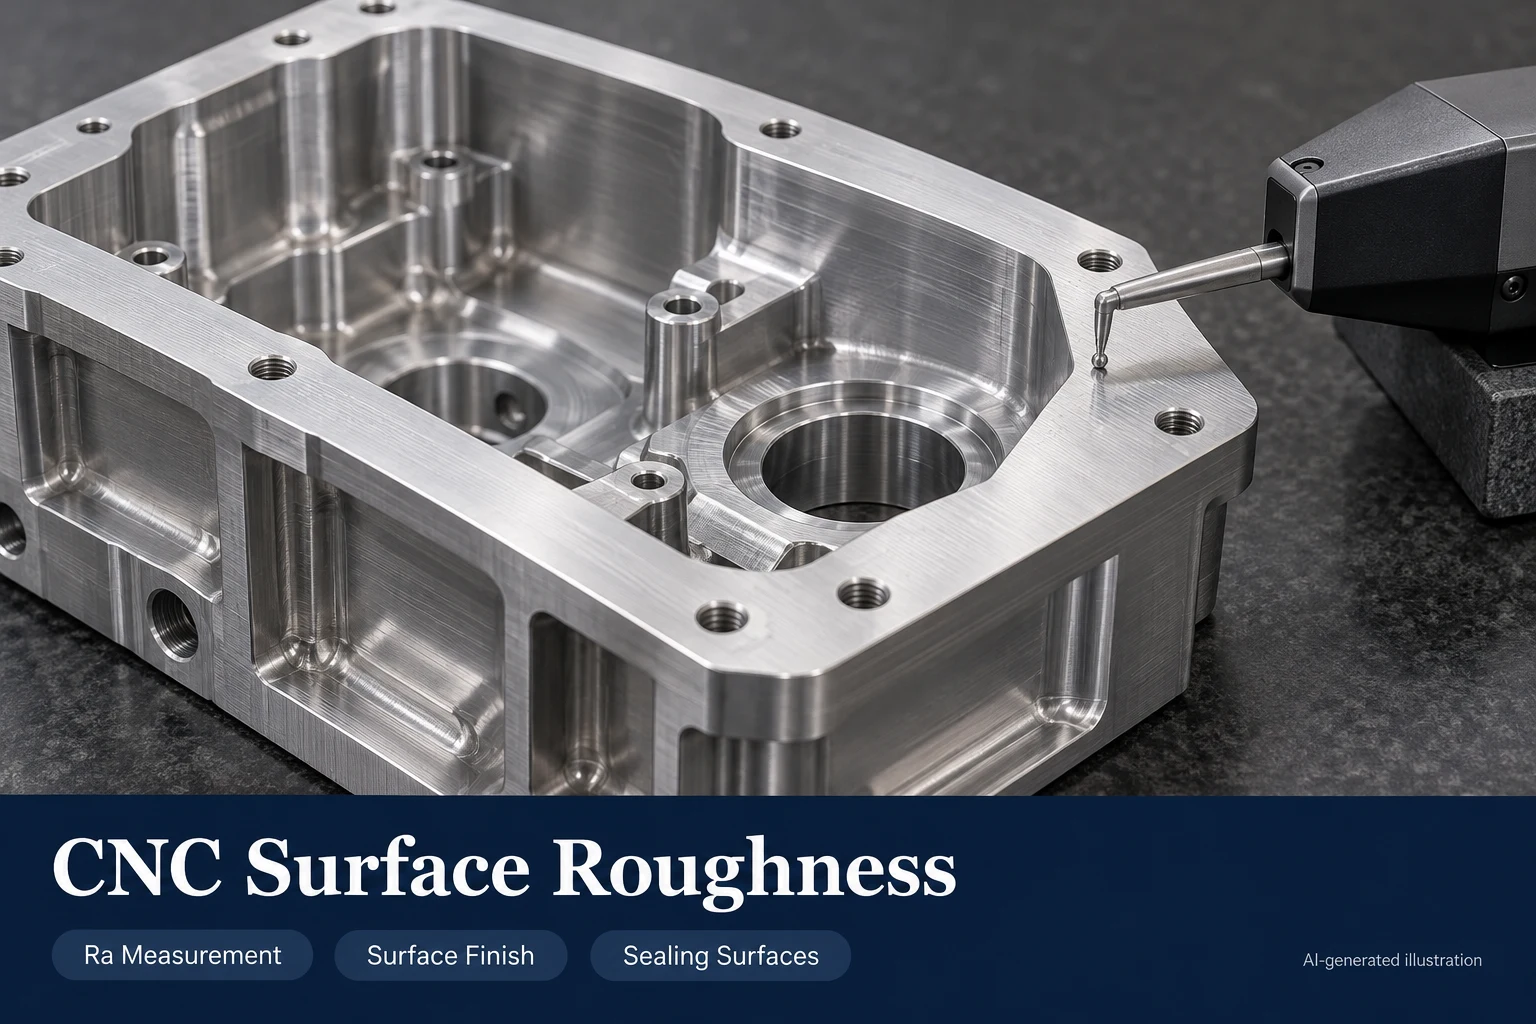
Surface Roughness in CNC Machining: Specify and Verify the Finish
Specify CNC surface roughness by function. Learn what Ra misses, how to agree on measurement conditions, and what to include in a finish inspection plan.
CNC Pilot Production Checklist: Approve the Batch Before Scaling
.lxc-blog{max-width:900px;margin:auto;color:#29343d;font-size:16px;line-height:1.8}.lxc-blog h2{font-size:27px;line-height:1.3;m...
CNC Boring Chatter: Diagnose Marks and Protect Precision Fits
.lxc-blog{max-width:900px;margin:auto;color:#29343d;font-size:16px;line-height:1.8}.lxc-blog h2{font-size:27px;line-height:1.3;m...