Blog

Your supplier sends a dimensional report marked “PASS,” but incoming inspection finds a fit problem. Before assuming either measurement is wrong, check whether both teams evaluated the same drawing revision, part, datum setup and feature. A useful CNC inspection report checklist connects each result to a requirement and a traceable sample; a green status alone does not establish that connection.
Why a dimensional inspection report can be difficult to accept
Reports can fail the purchasing team even when they contain many numbers. Common gaps include an obsolete drawing revision, unidentified samples, incomplete feature coverage, rounded values near a limit, or measurements made before a finish that affects the final dimensions. A report for one approved sample also does not automatically describe the entire shipment.
Procurement should coordinate the evidence requirement with engineering and quality. The purchase order can then identify the report deliverables, sampling basis, approval milestones and handling of nonconforming results. This prevents a disagreement about documentation after the parts have already shipped.
CNC inspection report checklist: review these fields first
| Report field | Evidence to request | Question before acceptance |
|---|---|---|
| Identity and revision | Part number, drawing revision, report date, order or batch reference and sample IDs | Does the report describe the supplied parts and current requirement? |
| Characteristic mapping | Numbered drawing features linked to report rows | Can each result be located unambiguously? |
| Limits and units | Nominal, upper/lower limits, units and relevant GD&T definition | Were the actual drawing requirements used? |
| Measured values | Individual results for the identified samples; disposition of exceptions | Is the PASS/FAIL status supported by the numbers? |
| Measurement method | Instrument or method, setup and relevant datum/evaluation information | Is the method suitable for the feature and acceptance decision? |
| Inspection scope | Sample quantity, selected features, production stage and exclusions | What does the report establish, and what remains unchecked? |
| Release status | Responsible review and approved deviation references where applicable | Are unresolved results clearly separated from accepted ones? |
Use a simple numerical review before trusting PASS/FAIL
Hypothetical example, not a production result: a bore specified as 10.00 ± 0.02 mm has limits of 9.98–10.02 mm. A reported value of 10.03 mm is outside those stated limits. Ask for correction or disposition if it is marked PASS. A value printed as “10.0” may lack enough displayed detail to assess a tight tolerance; request appropriately resolved results and the applicable measurement decision rule.
A result close to a limit requires more care than a simple arithmetic check. Instrument resolution is not the same as measurement uncertainty, and a calibration certificate alone does not describe every influence on a specific measurement. Ask quality personnel to review the method, uncertainty and agreed decision rule when acceptance is sensitive to these issues.
When supplier and incoming measurements disagree
First preserve the identity of the sample and compare the two methods. Check drawing revision, units, datum alignment, fixturing, measurement location, part temperature and whether burrs, contamination or surface treatment affect contact. For geometric tolerances, review the feature extraction and evaluation strategy instead of comparing only the final number.
ZEISS identifies environmental conditions, setup, probe behavior and measurement strategy as influences on CMM results. Its guidance also emphasizes connecting inspection definitions to the design. These points support a joint method review; they do not establish that any particular machine or report is sufficient for every part. Source: ZEISS, Common CMM Inspection Errors and How to Reduce Them.
Agree on a comparison procedure using the same identified sample. Ask each party to document its setup and results, then involve the responsible engineer or metrology specialist. Do not select whichever number is commercially convenient or silently average conflicting measurements.
Separate first-article evidence from batch acceptance
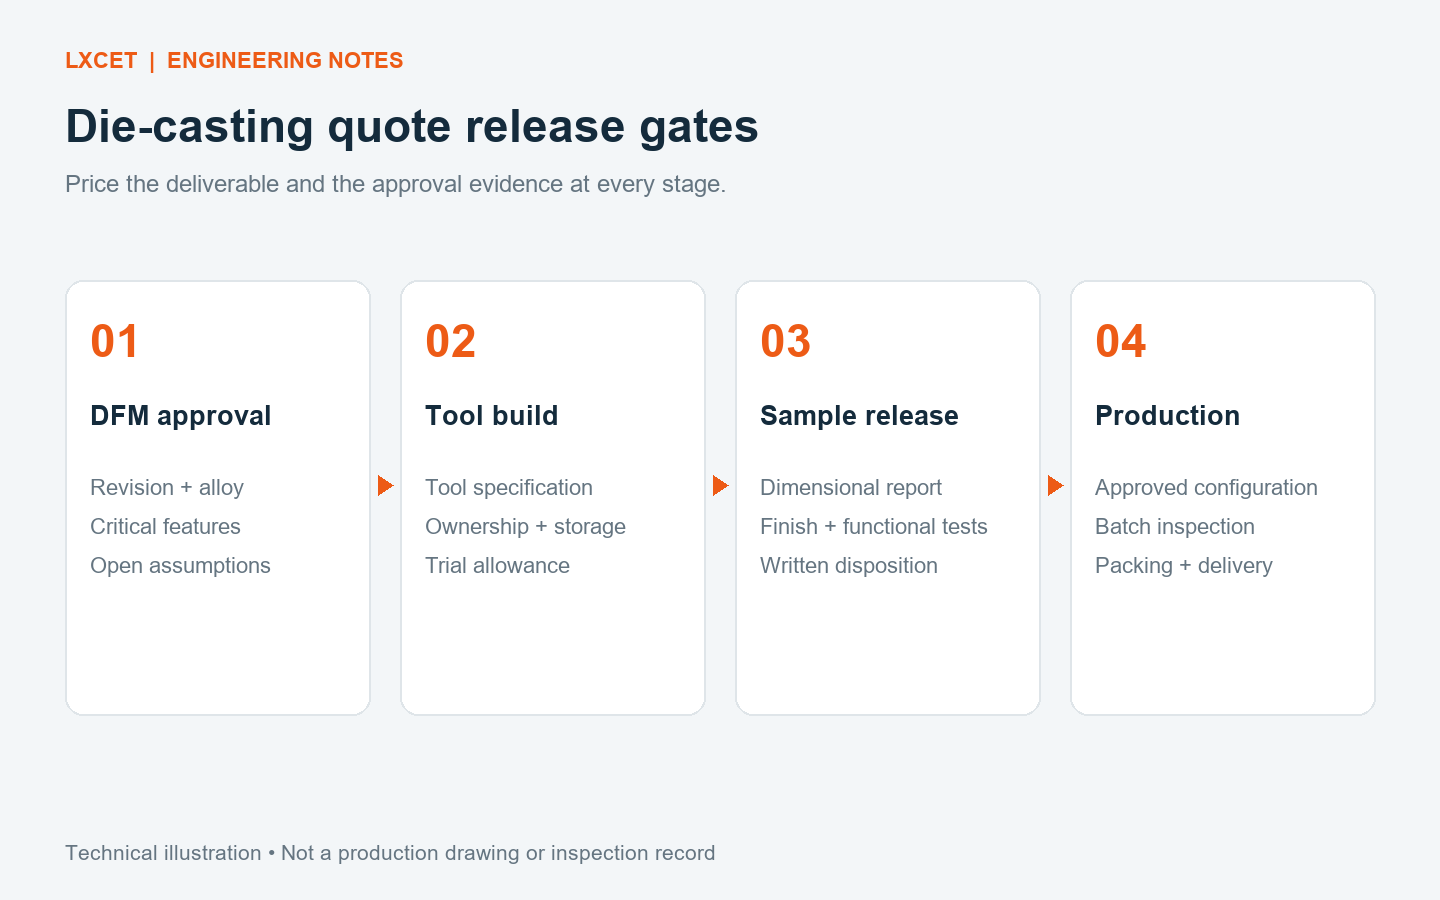
A first-article review checks the agreed initial sample scope. Batch acceptance needs its own sampling or inspection agreement and shipment traceability. Specify what must be checked after material, tooling, revision or process changes. If an industry-specific first-article format is required, name it in the order rather than assuming a general report meets that requirement.
ZEISS describes first-article inspection using a measurement plan, drawing or CAD with defined inspection information. Use those controlled inputs to agree on feature coverage. Source: ZEISS, First Article Inspection.
RFQ and purchase-order document checklist
- List required dimensional reports, material documents and special test records separately.
- Identify critical features, numbered characteristic coverage and the drawing revision.
- State sample quantity and whether measurements apply before or after finishing.
- Agree on report language, units, file format and required delivery timing.
- Define how exceptions, substitutions and deviations receive written approval.
- Confirm that the quoted price includes the agreed inspection and documentation scope.
Order the evidence alongside the parts
Send your drawing and required inspection deliverables to tonyzhou@lxcet.com for an LXCET project discussion. The actual inspection scope, equipment suitability and documentation are agreed for each project. Review our quality and inspection page, manufacturing solutions and RFQ comparison checklist before requesting a quotation.